In 2026, choosing a supplier for Precision Mold Components means looking beyond a polished catalog. A mold may depend on tiny details: a guide pin’s fit, a cavity insert’s finish, or a cooling channel’s position. One mismatch can cause extra adjustments, delayed trials, or inconsistent parts. Small dimensions matter.
Quality expert W. Edwards Deming offered a useful principle: “Quality comes not from inspection, but from improvement of the production process.” For mold components, that means asking how a supplier controls work—not just whether it provides an inspection report. Request material certificates, dimensional records, and clear tolerance data. Ask how the shop handles a nonconforming part. A useful answer should describe real checks, not vague promises.
Look for evidence of relevant machining experience, stable processes, and communication during design review. Share a drawing or sample specification and ask the supplier to identify risks before production. Check whether its equipment and measurement methods suit your component’s tolerances. Confirm lead times, revision control, packaging, and after-sales support. These details can reveal more than a low quotation.
No checklist removes every risk. A supplier may perform well on standard inserts yet struggle with a demanding custom geometry. Start with a technical discussion, then validate claims through records and a suitable sample order. Trust should be earned. The right partner helps protect fit, repeatability, and production schedules—and admits when a requirement needs clarification. That honesty matters, too.
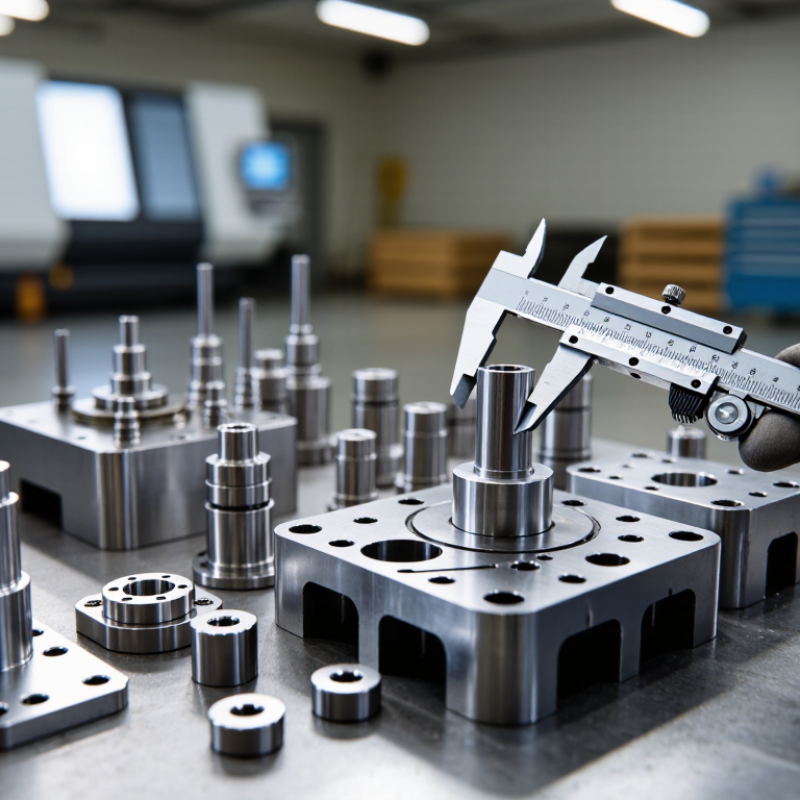
Precision mold components are the machined and fitted elements that locate, shape, support, or release material inside a mold. Their function matters more than their appearance. A guide pin, for example, keeps mold halves aligned during repeated closing cycles. Small parts, big effects.
Functional groups make component requirements easier to discuss. Guiding and locating parts include pins, bushings, and locating blocks. Forming parts, such as cores and cavities, create the product’s surfaces and dimensions. Ejection parts include pins and sleeves that push a molded part free. Cooling components carry temperature-control fluid through channels or fittings. Fasteners and wear plates hold assemblies together and protect areas exposed to friction. These categories can overlap; a component’s role depends on the mold design.
When comparing suppliers, match each part to its working conditions. A cavity insert may need careful surface finishing, while an ejector pin needs consistent diameter and straightness. Share current drawings, material requirements, heat-treatment needs, and inspection criteria. Ask how critical dimensions are measured, and request inspection records for important features. A category alone does not define quality. I would also check whether the supplier flags unclear tolerances before machining; drawings are not always as precise as their authors intend.
When comparing precision mold component suppliers, ask how they interpret fit callouts, not just whether they can hold a stated tolerance. ISO 286-1 explains the system of tolerances, deviations, and fits. ISO 286-2 provides tables for standard tolerance classes and limit deviations for holes and shafts. A tolerance grade indicates the permitted size variation; the fit designation combines that grade with a tolerance position. Small differences matter.
For a guide pillar and bushing, a callout such as H7/g6 commonly specifies a clearance fit. Confirm that the fit suits the component’s movement, lubrication, material, and operating temperature. State the nominal diameter and fit on the drawing, and identify any surfaces that need special attention. Avoid applying a tight grade everywhere. It can raise cost without improving mold performance.
Ask suppliers for inspection results on critical diameters, including actual measured values and the measurement method. Their equipment should suit the tolerance: a micrometer or calibrated bore gauge may be more useful than a quick visual check. Request samples or first-article measurements for key sliding parts. Still, a precise callout can create false confidence if alignment and assembly conditions are ignored. That detail is easy to miss. Revisit the fit after testing, especially if the component binds or shows uneven wear.
Standard tolerance widths for nominal sizes over 18 mm up to and including 30 mm. Smaller IT grades indicate tighter dimensional tolerances.
ISO 286-1 defines the system of limits and fits, while ISO 286-2 provides standard tolerance values and limit deviations. These values show tolerance width—not clearance or interference. For a mold component, specify the nominal size, hole and shaft tolerance designations (for example, H7/g6 where appropriate), and verify the supplier’s inspection method and measurement records.
2026 How to Find Precision Mold Components Suppliers
Screen Suppliers for ±5 μm Capability and Traceable CMM Inspection
A ±5 μm claim needs context. Ask which dimensions meet that tolerance, on which materials, and under what conditions. A supplier should explain datum selection, measurement uncertainty, and how parts are stabilized before inspection. Request a recent CMM report tied to a part number, revision, and production lot. Check whether the reported results cover critical features, not just easy-to-measure surfaces. A machine specification alone proves little.
Tips: Ask for a sample report with identifying details removed. Confirm the CMM’s calibration status and the inspection date. Compare a few reported dimensions with your drawing, including units and datum references. Small gaps matter.
During a supplier review, look for a repeatable process: documented inspection steps, controlled temperature, and records that link measurements to the delivered batch. Ask how out-of-tolerance results trigger investigation and corrective action. If possible, send a representative component for a trial inspection. One polished report is not enough; it may not reflect routine production. Even a careful checklist can miss setup variation, so agree on measurement methods before approval.
2026 How to Find Precision Mold Components Suppliers
Precision mold components often look interchangeable on a drawing. In production, a few microns of mismatch can affect fit, wear, and cycle stability. ISO 9001:2015 Clause 8.4 requires organizations to control externally provided processes, products, and services. It also calls for criteria to evaluate, select, monitor, and re-evaluate suppliers. ISO’s 2022 Survey of Management System Standard Certifications recorded more than one million valid ISO 9001 certificates worldwide. That figure shows broad adoption, not proof that any individual supplier can hold a tight tolerance.
During an audit, ask how the supplier controls outsourced grinding, heat treatment, and coating. Request recent inspection records for a comparable component, not only a polished sample. Check whether CMM calibration is current, material certificates match the purchase order, and nonconforming parts are traced by lot. A useful supplier review connects each risk to evidence: audit findings, corrective-action records, and delivery performance. Clause 8.4 also expects controls to reflect the potential impact of supplied work on final product quality.
A certificate is a starting point. It is not a shortcut. One uncomfortable detail: supplier scorecards can hide recurring defects when data is averaged across many part numbers. Review a specific mold insert or ejector pin, then ask what changed after the last failure. A missing record matters, too. Note it, agree on a corrective action, and verify closure before increasing order volume.
| ISO 9001:2015 Reference | Audit Dimension | What to Verify for Mold Components | Objective Evidence to Sample | Evaluation Guide |
|---|---|---|---|---|
| 8.4.1 | Supplier selection and approval | Confirm selection criteria consider the supplier’s ability to meet drawing, material, dimensional, delivery, and applicable regulatory requirements. | Approved supplier criteria, initial evaluation records, technical capability review, and approval status for the relevant component category. | Acceptable when documented criteria are applied before purchase and approval is traceable to the supplier and scope of supply. |
| 8.4.1 | Monitoring and re-evaluation | Check that supplier performance is monitored and re-evaluation is performed at planned intervals or when performance issues arise. | Incoming inspection results, delivery performance records, nonconformity and corrective-action history, and dated re-evaluation records. | Acceptable when monitoring results inform decisions and action is taken when performance does not meet requirements. |
| 8.4.2 | Type and extent of control | Verify controls are proportionate to the component’s impact on conformity and to the effectiveness of the supplier’s own controls. | Risk-based inspection plans, supplier process assessments, receiving inspection records, and defined verification or testing activities. | Acceptable when higher-risk or critical characteristics receive appropriate verification and control methods are defined. |
| 8.4.2 | Verification of purchased components | Check that verification confirms conformity to the current specification, including applicable dimensions, material, hardness, surface finish, and heat-treatment requirements. | Inspection reports, certificates or test reports when specified, calibrated measurement equipment records, and links to the applicable drawing revision. | Acceptable when verification methods and acceptance criteria are established and records identify the inspected lot or part. |
| 8.4.2 | Control of changes | Determine whether changes affecting supplied components, processes, materials, or manufacturing location are reviewed and authorized as required. | Change notifications, customer or internal approvals where required, revised specifications, and records showing implementation dates or affected lots. | Acceptable when relevant changes are controlled and the organization can assess their effect before use. |
| 8.4.3 | Clarity of purchasing requirements | Confirm purchase information adequately describes the component and applicable requirements, including drawing revision, material specification, quantity, and acceptance criteria. | Purchase orders, technical specifications, controlled drawings, quality clauses, and records showing requirements were reviewed before communication to the supplier. | Acceptable when requirements are complete, current, and communicated before the supplier accepts the order. |
| 8.4.3 | Competence and external provider interactions | Where relevant, communicate competence requirements, required interactions, inspection or approval activities, and any intended verification at the supplier’s premises. | Order requirements, supplier instructions, inspection arrangements, approval records, and agreed access or verification provisions. | Acceptable when applicable requirements are communicated and agreed arrangements are documented. |
| 8.4.3 | Nonconformity communication and response | Verify that nonconforming supplied components are identified, contained, and communicated, with corrective action requested when appropriate. | Nonconformity reports, containment records, supplier responses, corrective-action evidence, and disposition approvals. | Acceptable when affected product is controlled and actions are followed through to a documented disposition and effectiveness review when required. |
Audit note: Use this checklist as a practical review aid. The applicable controls and sampling depth should reflect the organization’s requirements, risks, and the intended use of the externally provided components.
A 2026 search for precision mold components suppliers should start with a like-for-like request for quotation. Send each supplier the same drawing revision, quantity, tolerance schedule, and delivery destination. Ask for the exact material grade, not just “tool steel” or “stainless steel.” Request a mill certificate linked to the quoted stock, plus any heat-treatment records. Small differences matter. A hardness range that looks acceptable on paper may still affect wear or machining.
Compare lead times as dated milestones: material availability, machining, heat treatment, inspection, and dispatch. Ask whether the quoted date includes approval of first-article results. For inspection evidence, request a dimensional report tied to drawing characteristics, with actual readings, units, and instrument identification. A clear report might show a 20.00 mm bore measured at 19.99 mm, rather than simply marking it “pass.” Check whether critical features receive full inspection or sampling. Then compare landed cost, including packaging and shipping, not only the unit price. A neat quotation can still hide a weak assumption; confirm what happens if material availability slips. My own checklist would not catch every shop-floor constraint, so discuss unusual geometry directly with the supplier’s engineer.